

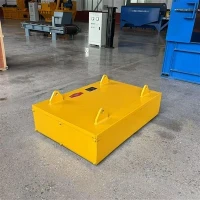


Reliable Conveyor Belt Metal Detector
What Is a Conveyor Belt Metal Detector?

A conveyor belt metal detector is an industrial detection system installed above or around a conveyor belt to continuously monitor bulk materials during transportation. It identifies unwanted ferrous and non-ferrous metal contaminants hidden inside ores, coal, limestone, aggregates, cement raw materials, and other bulk products before they reach crushers, mills, or other downstream equipment.
The GJT-B Belt Metal Detector adopts advanced digital phase-shift detection technology to deliver high detection accuracy, strong anti-interference capability, and stable long-term performance in demanding industrial environments.
Why Metal Detection Is Important
Metal fragments introduced during mining, excavation, transportation, or loading can cause severe damage to crushers, grinding mills, conveyor belts, and screening equipment. Even a small piece of tramp iron can result in equipment failure, costly repairs, and unplanned production shutdowns.
By detecting metal contaminants in real time, industrial metal detectors help operators remove hazardous objects before they enter critical processing equipment, reducing maintenance costs and extending equipment service life.

Key Advantages of the GJT-B Belt Metal Detector
The GJT-B Belt Metal Detector is designed to provide reliable and continuous protection for bulk material conveying systems.
Its major advantages include:
High sensitivity for detecting both ferrous and non-ferrous metal contaminants.
Advanced digital signal processing for accurate and stable detection.
Excellent resistance to electrical noise, vibration, and harsh industrial conditions.
Continuous online monitoring without interrupting material transportation.
Adjustable sensitivity to match different conveyor widths and material characteristics.
Fast alarm and control signal output for immediate system response.
Rugged industrial construction for long service life and low maintenance.
Easy integration with conveyor belts, crushers, and automatic control systems.
Typical Applications
The GJT-B Belt Metal Detector is widely used in industries that transport bulk materials through conveyor systems, including:
Mining and mineral processing
Coal preparation plants
Cement manufacturing
Quarry and aggregate production
Metallurgical processing
Thermal power plants
Port and bulk cargo terminals
Recycling facilities
Building material production
Chemical processing plants
Conclusion
As industrial production continues to move toward greater automation and higher efficiency, conveyor belt metal detection has become an essential part of bulk material handling systems. The GJT-B Belt Metal Detector combines advanced detection technology, high sensitivity, and dependable industrial performance to help manufacturers protect valuable equipment, improve production safety, and reduce operating costs. Whether used in mining, cement, coal, metallurgy, or aggregate processing, it provides a reliable and cost-effective solution for continuous online metal detection.
Hot Tags: reliable conveyor belt metal detector, China reliable conveyor belt metal detector manufacturers, suppliers, factory, best metal detector, conveyor metal detectors, conveyor type metal detector, Frame Type Metal Detector, magnetic metal detector, metal detecting equipment
Previous
No InformationYou Might Also Like


Send Inquiry